 en
 English
 中文简体
 Español
 русский
 Français
 عربى
 Deutsch
 Português
 日本語
 한국어
 italiano
Shengya
Shengya
Shengya
Shengya
Shengya
Shengya
Shengya
Shengya
Shengya
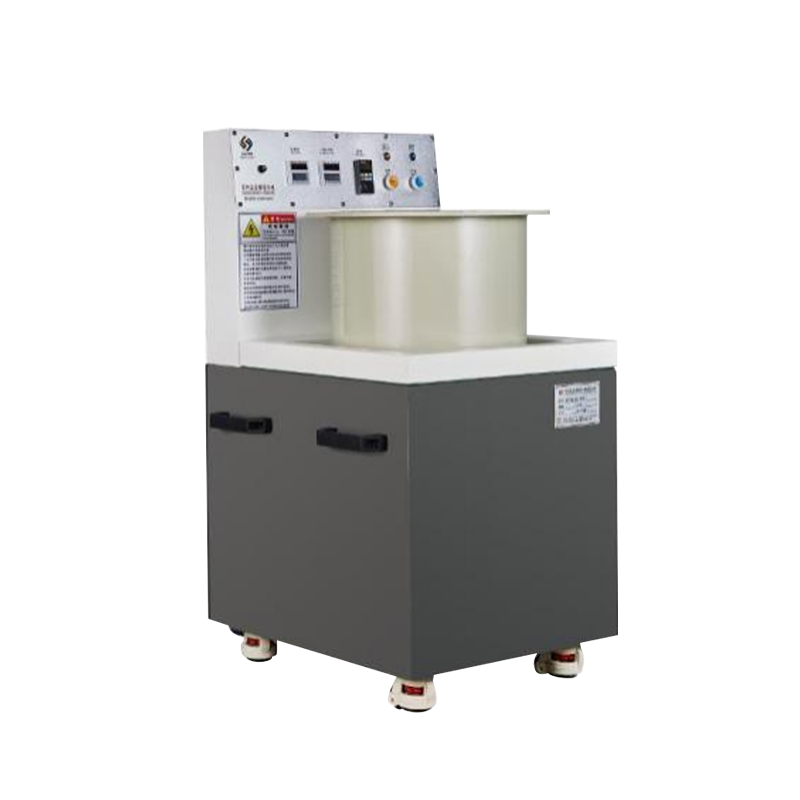

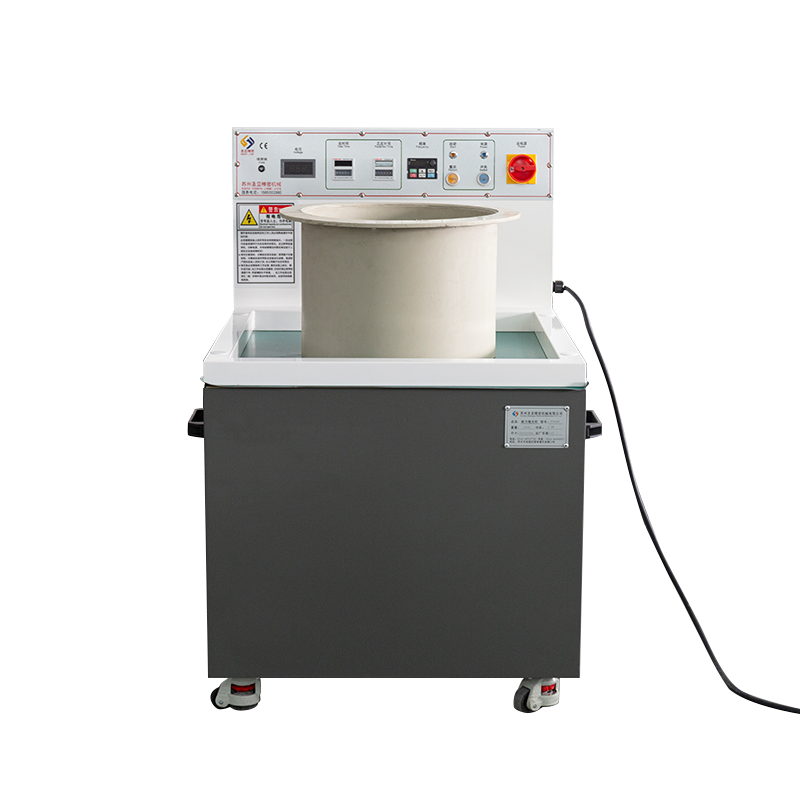
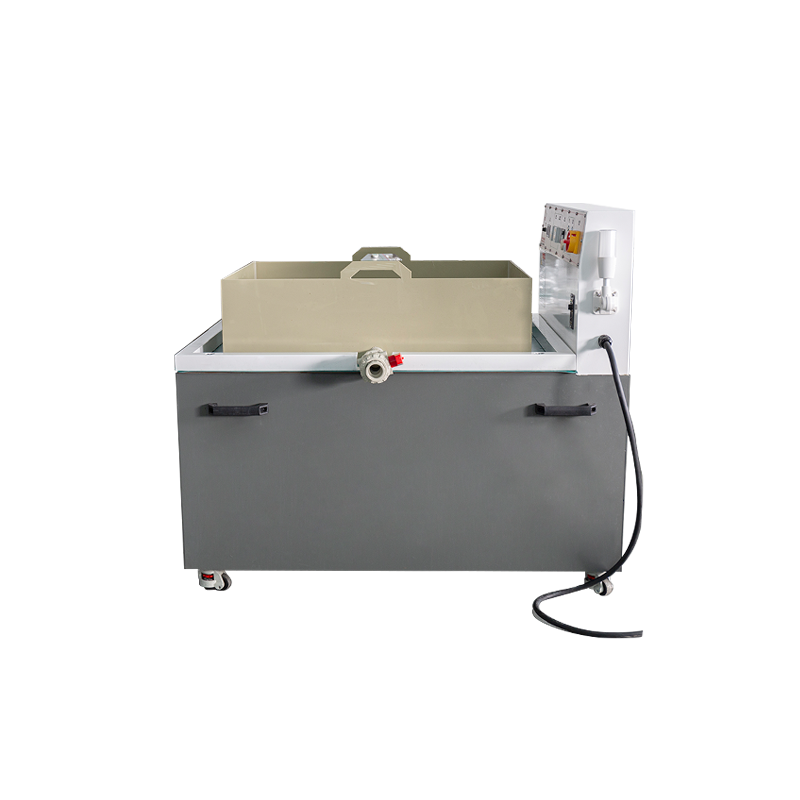
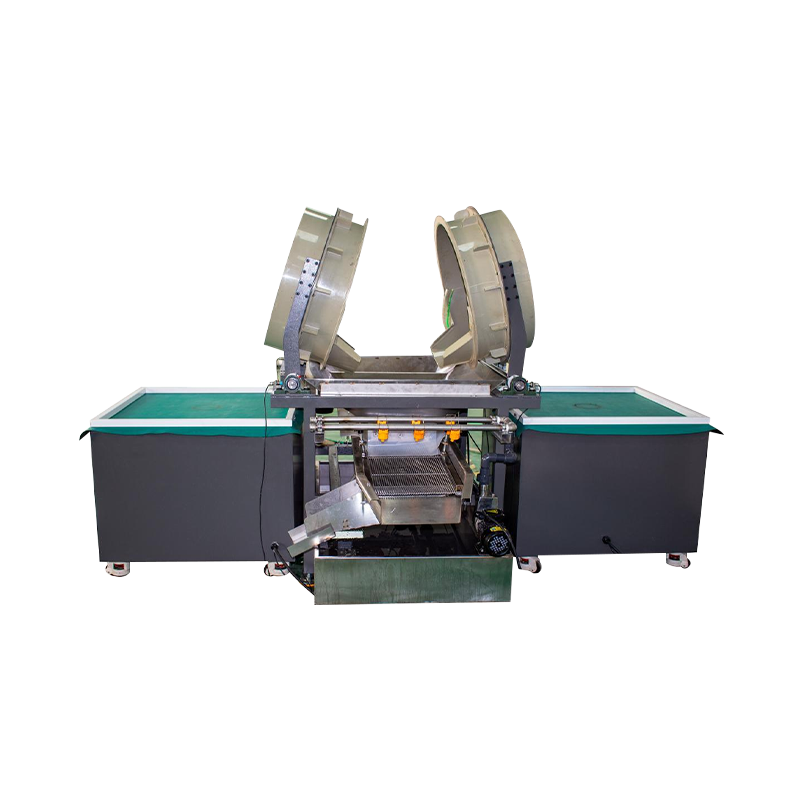
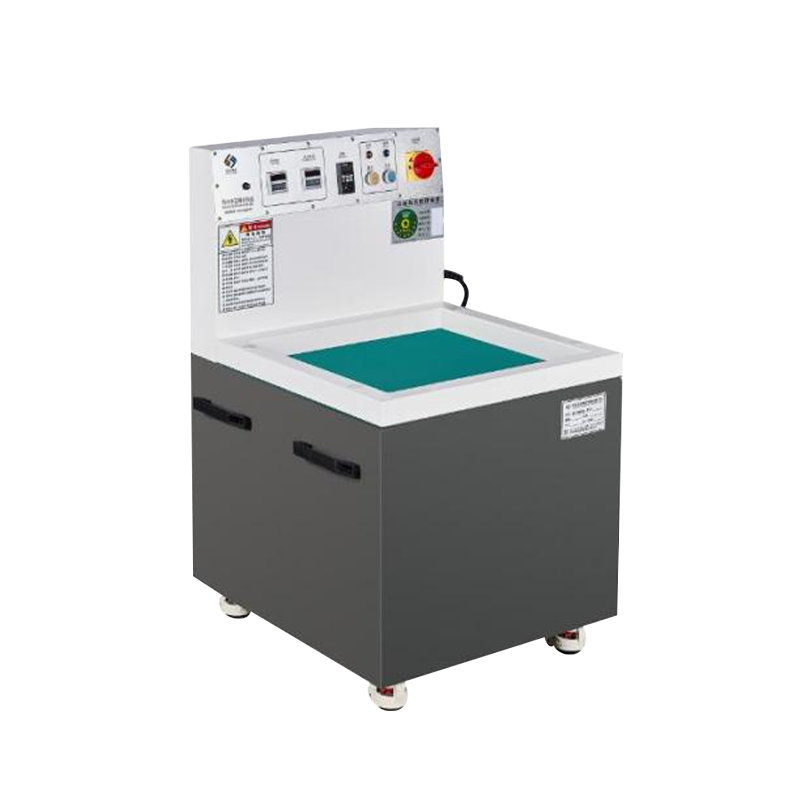
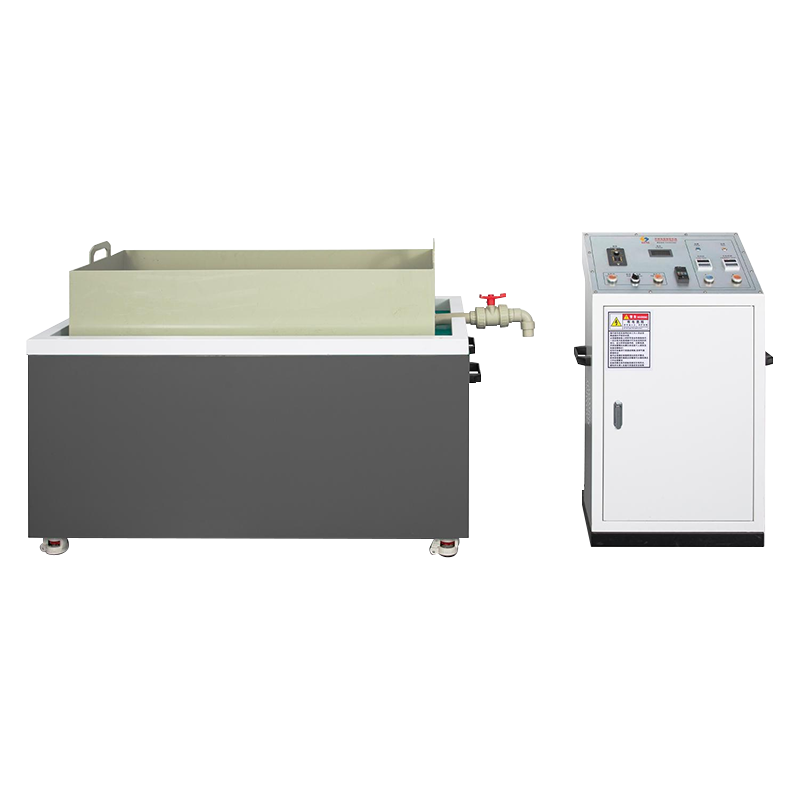
Specification
| Parameter | Typical Specification |
|---|---|
| Working principle | Rotating magnetic field drives stainless steel pins through the part surface |
| Pin material | SUS304 or SUS316 stainless steel |
| Pin diameter | 0.2 mm to 1.5 mm, selected by burr size and part geometry |
| Tank capacity | 1 L to 6 L, bench-top models suited to small parts |
| Rotation speed | Approx. 500 to 2800 rpm, stepless adjustment |
| Motor power | 0.4 kW to 1.5 kW depending on model |
| Power supply | 110 V / 220 V / 380 V, 50 / 60 Hz, customizable to destination market |
| Process time | Typically 10 to 60 minutes per batch |
| Process medium | Clean water with a deburring or polishing liquid |
| Control | Digital timer and speed control; forward / reverse rotation on selected models |
| Optimal part size | 0.5 mm to 30 mm |
| Recommended pin size | 0.2 mm to 0.5 mm |
| Speed control | Stepless adjustment for gentle to aggressive action |
| Typical process time | 5 to 30 minutes for micro parts |
| Suitable materials | Stainless steel, titanium, brass, copper, aluminum, precious metals |
Specifications are typical values. Models, tank size, voltage and options can be customized. Please contact us with your part details for a suggested configuration.
Application
This machine suits industries where parts are tiny, tolerances are tight and surface quality matters.
- Micro screws and pins: clean threads and heads in bulk.
- Electronic connector contacts: remove burrs from small pins and terminals.
- Watch and instrument parts: finish gears, springs and fine components.
- Medical micro components: polish small needles, tips and fasteners.
- Sensor and optical housings: deburr small bores and edges.
- Swiss-machined micro parts: finish very small parts directly from the machine.
For very small lots, we recommend sending a sample set so we can match the pin size and process time before you order.
Advantages
- Very fine control: tiny pins and precise speed steps protect delicate geometry.
- Micro-hole access: pins reach into holes where larger media cannot enter.
- Better surface quality: removes burrs and leaves a uniform polished look.
- Low scrap rate: soft action avoids deformation and chipping.
- Quick cycle: most micro parts are finished within minutes.
- Bench-top convenience: small footprint suits labs, cleanrooms and workshops.
Comparison with Other Deburring Methods
| Factor | Magnetic Pin Deburring | Vibratory or Barrel Finishing | Manual Deburring |
|---|---|---|---|
| Access to small holes and slots | Excellent, fine pins enter micro features | Limited, media is often too large | Depends on operator and tools |
| Typical cycle time | 10 to 60 minutes per batch | Several hours per batch | Minutes per part, labour heavy |
| Consistency between batches | High, controlled by time and speed | Medium | Varies by operator |
| Risk of part-to-part damage | Low, parts are held in the pin bed | Higher, parts can collide | Scratches and over-removal possible |
| Labour requirement | Low, load and unload only | Low | High |
| Fit for micro parts | Pins as fine as 0.2 mm | Media too large, parts may trap | Difficult under magnification |
Buyers usually compare cycle time, access to small features, running cost and consistency. Send us a sample and we can show how the process performs on your own parts.